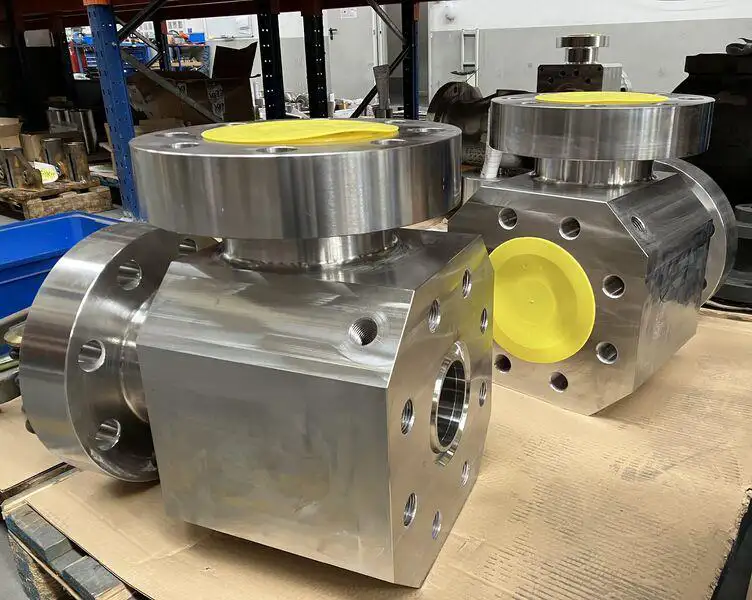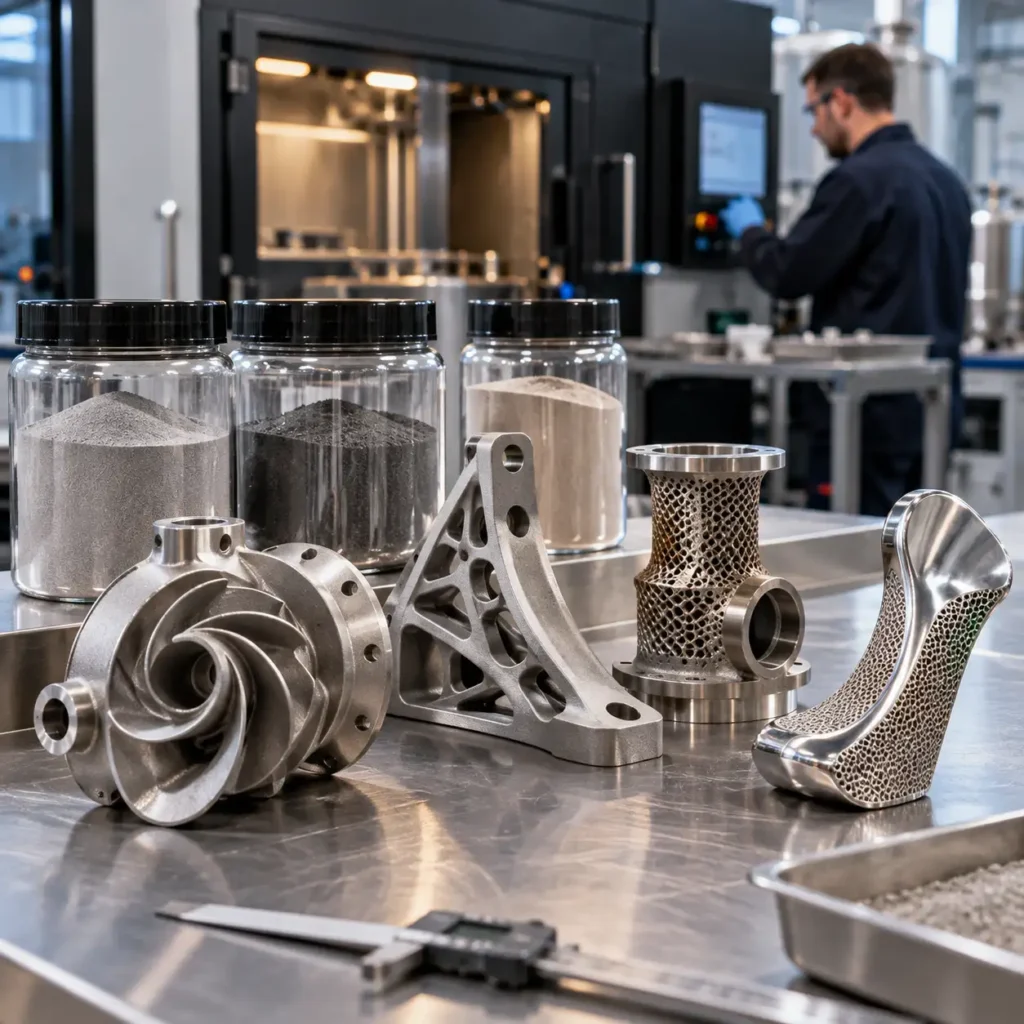
Oil and gas equipment must operate within demanding mechanical, hydraulic and environmental conditions. Pumps, valves, manifolds and other flow-handling components may be exposed to pressure fluctuations, corrosive fluids, erosion, elevated temperatures and repeated operating cycles.
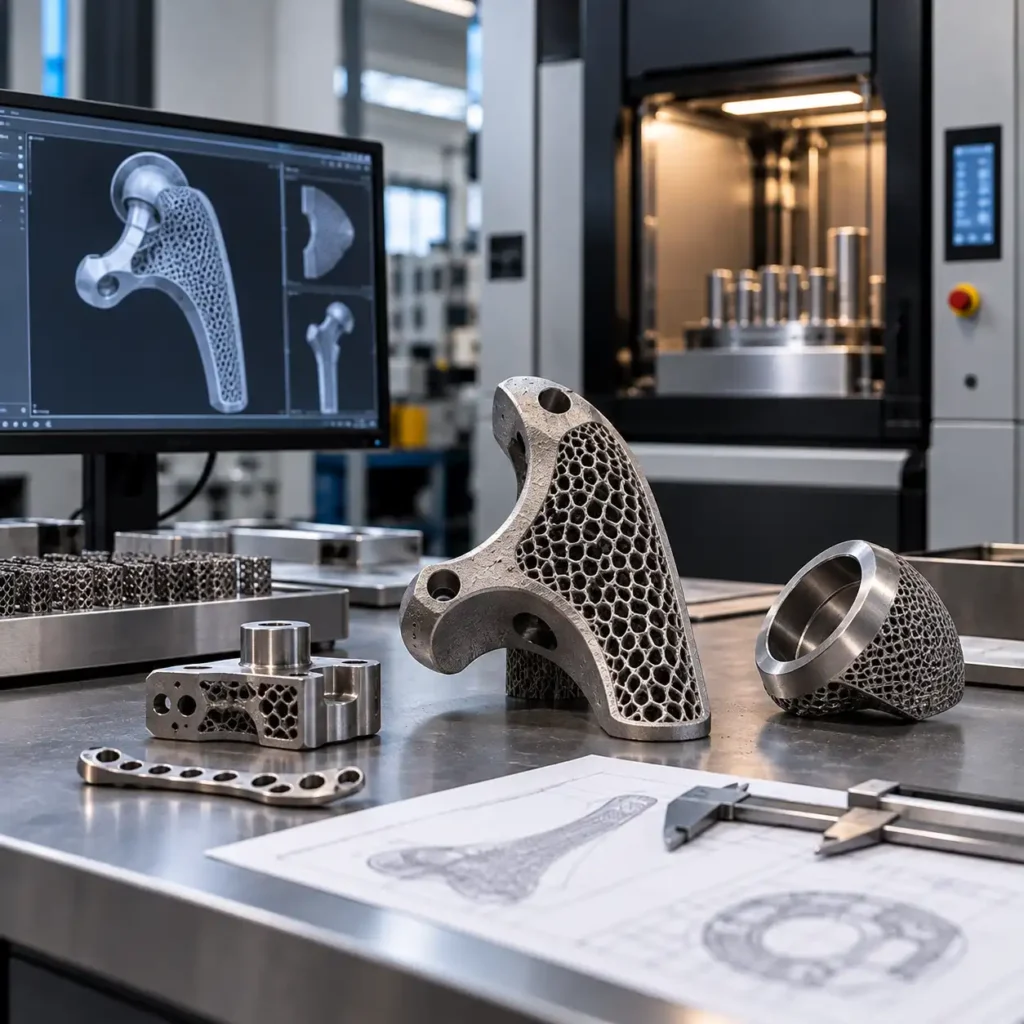
Metal additive manufacturing provides an alternative manufacturing route for selected components, particularly where complex geometries, integrated internal passages or specialised low-volume designs are difficult to produce using conventional methods.
For oil and gas engineering teams, however, the central question is not simply whether a component can be printed. It is whether additive manufacturing can deliver a technically suitable component that can be manufactured consistently, inspected adequately and qualified for its intended service.
This guide examines the engineering opportunities and limitations of metal additive manufacturing for pumps, valves and flow components, with particular attention to Laser Powder Bed Fusion (LPBF), material selection, design optimisation, post-processing and component qualification.
Why Consider Metal Additive Manufacturing for Oil and Gas Components?
Conventional manufacturing processes—including casting, forging, machining and fabrication—remain essential to the oil and gas industry. They are well established for many standard components and may offer lower costs, established supply chains and proven qualification pathways.
Metal additive manufacturing becomes relevant when a component’s geometry, production requirements or design constraints create an opportunity that conventional processes cannot address as efficiently.
Potential opportunities include:
- Complex internal passages that are difficult to drill or machine.
- Integrated manifolds that could reduce the number of separate parts and connections.
- Specialised hydraulic geometries requiring design flexibility.
- Low-volume components for which dedicated tooling may be uneconomical.
- Prototypes used to evaluate alternative flow paths or component configurations.
- Selected replacement components that can be redesigned and qualified for additive production.
These are potential applications, not universal advantages. A complex geometry may be printable but difficult to clean, inspect or finish. A conventional casting may remain the better option for a large, relatively simple housing.
The strongest business case emerges when a specific manufacturing constraint can be connected to a measurable engineering or operational benefit.
Metal Additive Manufacturing for Pump Components
Pump performance depends on the interaction between impeller geometry, fluid properties, rotational speed, operating conditions and the surrounding hydraulic system. Additive manufacturing can provide additional geometric freedom when engineers develop or revise selected pump components.
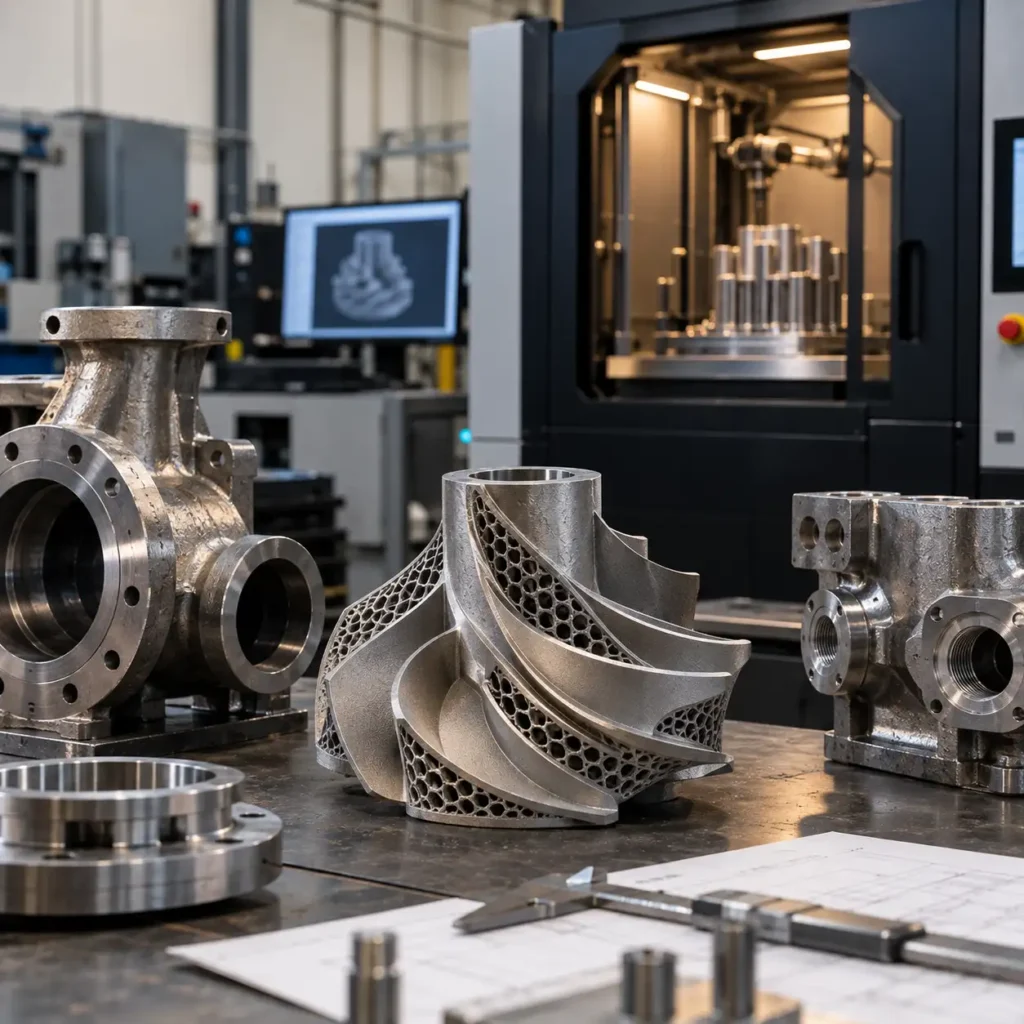
Impellers and complex hydraulic geometries
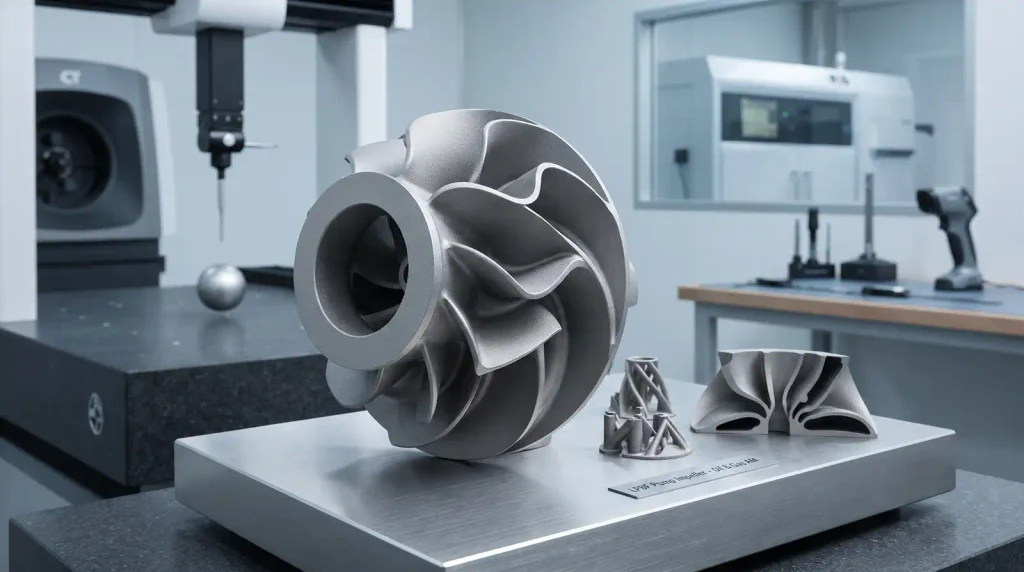
An impeller’s blades, hub and flow passages determine how energy is transferred to the fluid. Depending on the pump design, these features may involve curved surfaces and complex transitions that are difficult to machine using conventional tools.
LPBF can produce certain geometries without requiring all the tooling, access directions or assembly operations associated with conventional production.
Possible design investigations include revised blade profiles, integrated features and geometries developed through computational fluid dynamics (CFD).
However, a printable impeller is not automatically a high-performing impeller. Its hydraulic behaviour must be evaluated against the intended duty point, fluid properties, operating speed and system requirements.
Surface roughness is particularly important. As-built LPBF surfaces may differ substantially from the smooth surfaces assumed in an idealised CAD model or CFD simulation. Additional finishing, machining allowances or design adjustments may be necessary.
Structural integrity and rotating equipment
Pump impellers and other rotating parts require attention to fatigue, dynamic balance, dimensional tolerances and defect sensitivity.
Build orientation, support strategy, thermal distortion, residual stress, heat treatment and post-build machining should be considered before the component enters production.
The assessment should also consider the consequences of component failure. A non-critical prototype and a rotating part intended for demanding industrial service do not require the same evidence of conformity.
For production applications, material properties, manufacturing consistency, inspection and appropriate performance testing must be evaluated alongside geometric accuracy.
Additive Manufacturing for Valve Bodies and Flow Control Components
Valve-related components combine fluid control functions with mechanical and, in some cases, pressure-retaining requirements. Their internal geometry may include intersecting bores, cavities, changes in flow direction and connections to surrounding equipment.
Conventional casting, forging and machining remain highly relevant to valve manufacture. LPBF is most compelling when a specialised design requires geometry, integration or production flexibility that justifies the additional process and qualification effort.
Redesigning internal flow passages
Additive manufacturing can allow engineers to investigate alternative passage layouts and transitions between connected channels.
Depending on the application, a revised geometry may help address local flow separation, recirculation or pressure losses. These outcomes must be demonstrated rather than assumed.
CFD can help compare design alternatives by examining velocity fields, pressure distribution and other relevant flow characteristics. The usefulness of the results depends on the model assumptions, boundary conditions, mesh quality and representation of the manufactured surfaces.
If the actual internal surface is rougher than the model assumes, predicted pressure losses and flow behaviour may differ from the final component’s performance.
A design review should therefore consider both the ideal geometry and the realistic manufacturing outcome.
Pressure-retaining boundaries and sealing interfaces
Valve bodies and other pressure-retaining components require more than dimensional conformity.
Depending on the component and its service conditions, acceptance may require evidence relating to material properties, defect control, pressure integrity, traceability and applicable design and manufacturing requirements.
Flange faces, sealing interfaces, threads and precision bores commonly require post-build machining. Internal porosity, lack-of-fusion defects and surface-connected discontinuities may be important where leakage, fatigue or structural failure is a concern.
The fact that a pressure-retaining component can be printed does not establish that it is suitable for pressure service. The design, manufacturing route, inspection plan and acceptance criteria must be established for the specific application.
Complex Manifolds and Internal Flow Channels
Complex manifolds provide one of the clearest examples of the geometric flexibility available through LPBF.
A conventionally manufactured manifold may require intersecting drilled passages, cross-drilling, plugs, fittings or several assembled components. An additively manufactured design may allow the passage network to be integrated more directly into a single body.
Component integration and design flexibility
Where the application supports it, component consolidation may reduce the number of separate parts, assembly operations or external connections.
Fewer interfaces can simplify assembly and may reduce some potential leakage paths. Nevertheless, integration does not remove the need to verify pressure integrity, flow performance or maintainability.
The engineering assessment should also account for the disadvantages of consolidating multiple functions into one component. A more integrated part may be harder to repair, inspect or replace if a local feature fails.
The challenge of enclosed passages
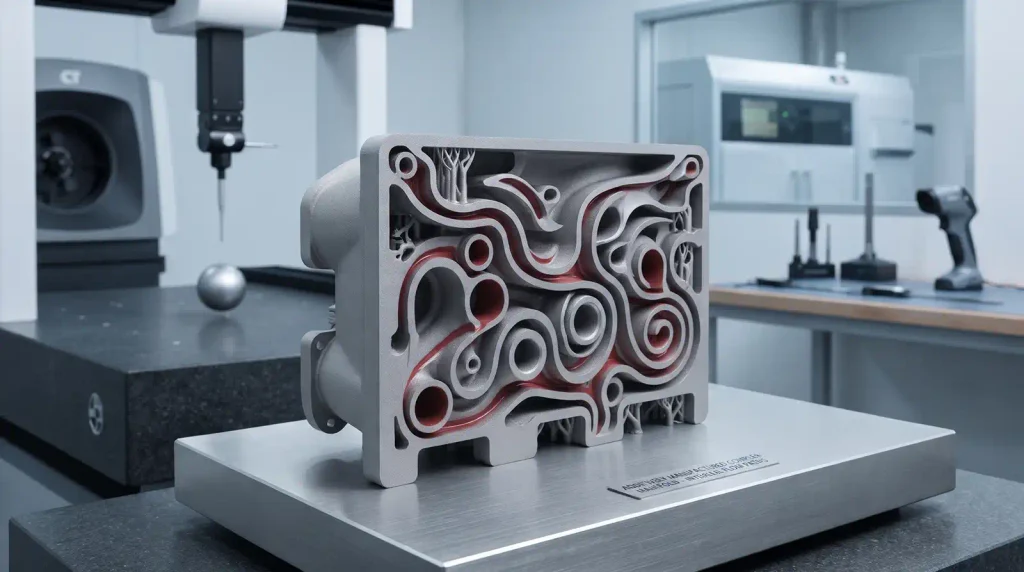
Internal passages introduce manufacturing and inspection constraints that are easy to overlook during CAD design.
Depending on channel dimensions, orientation and geometry, problems may include trapped powder, inaccessible surfaces, difficult support removal and limited access for conventional machining or finishing.
The design must therefore address four questions before the geometry is finalised:
- Can the passage be manufactured reliably within the selected process limits?
- Can residual powder and other unwanted material be removed?
- Can the required surface condition be achieved?
- Can the finished passage be inspected and its conformity verified?
Channel cross-sections, orientation, access openings and support requirements should be considered during Design for Additive Manufacturing (DfAM). Self-supporting geometries may reduce the need for internal supports in some designs, but they still require evaluation for flow performance and manufacturability.
A passage that cannot be cleaned and verified adequately should not be accepted merely because it appears feasible in CAD.
Design for Additive Manufacturing: Balancing Flow and Structural Performance
The most useful LPBF designs are not necessarily direct copies of conventionally manufactured components. In suitable applications, engineers can redesign geometry around additive manufacturing while preserving the component’s functional and mechanical requirements.
Computational fluid dynamics
CFD can support the investigation of pressure distribution, velocity, recirculation and potential areas of excessive flow resistance.
For a meaningful comparison, the model should represent the intended operating conditions and account for assumptions about surface roughness and manufactured geometry. A simulation of an idealised passage is not, by itself, evidence that the physical component will achieve the same result.
Where performance is critical, simulation should be supported by appropriate validation or physical testing.
Finite Element Analysis
Finite Element Analysis (FEA) can help evaluate stress distribution, deformation and loading under defined conditions.
Depending on the application, the assessment may need to consider pressure loading, thermal expansion, vibration, cyclic loading and fatigue. Additive manufacturing introduces further considerations, including process-dependent material properties, anisotropy and defect sensitivity.
Analysis should use assumptions and material data appropriate to the selected manufacturing route and material condition. It should not be treated as a substitute for manufacturing qualification or required testing.
Manufacturing constraints must influence the design
A geometry that performs well in CFD and FEA may still be impractical to manufacture.
LPBF feasibility depends on build volume, orientation, supports, thermal behaviour, powder evacuation, surface finishing and subsequent machining. These constraints should be evaluated early, before substantial effort is invested in optimising a geometry that cannot be produced or inspected as intended.
For further guidance on geometry, build orientation and support strategy, consult E-Metal3D’s engineering guidance on Design for Metal Additive Manufacturing.
Material Selection for Oil and Gas Applications
Material selection should begin with the actual service environment, not simply with the alloys available for a particular printer.
Oil and gas components may encounter chloride-bearing fluids, elevated temperatures, abrasive particles, cyclic loading and chemically aggressive conditions. Suitability depends on the material’s composition, microstructure, manufacturing condition, post-processing and applicable service requirements.
Stainless steel alloys
316L stainless steel is available for many metal powder bed fusion systems and is considered for a range of corrosion-resistant industrial applications.
Its suitability depends on the fluid chemistry, temperature, loading and relevant corrosion mechanisms. It should not be assumed suitable for every chloride-rich or sour-service environment.
Nickel-based alloys
Nickel-based alloys such as Inconel 625 and Inconel 718 are used in demanding engineering applications, but their properties and corrosion behaviour differ.
The appropriate choice depends on the intended function, operating environment and properties achieved through the selected manufacturing and heat-treatment route. An alloy’s performance in conventionally manufactured form does not automatically establish the performance of an additively manufactured component.
Material qualification and traceability
Powder chemistry, handling, reuse practices, process parameters, build orientation, heat treatment and inspection can influence the final component’s properties.
For demanding applications, the manufacturing plan may require representative material testing, traceability records and evidence that the process consistently achieves the specified characteristics.
Where sour-service or other restrictive material requirements apply, these must be assessed against the relevant standards and service conditions. Availability of a printable alloy does not demonstrate compliance.
For a broader comparison of industrial alloys, see E-Metal3D’s guide to Metal 3D Printing Materials in Australia.
Post-Processing and Surface Finishing
LPBF is usually one stage within a broader manufacturing route. Depending on the component, subsequent operations may include stress relief, heat treatment, removal from the build plate, support removal, machining, surface finishing and cleaning.
For pumps and flow components, surface condition can directly affect function. Hydraulic surfaces may require improved roughness, while sealing faces, precision bores, threads and connection features generally require controlled finishing.
Internal channels are more difficult because conventional tools may not reach them. The available finishing methods must be assessed against channel accessibility, material, geometry and the required surface condition.
No single finishing method should be assumed to produce a uniform result throughout every enclosed passage. Where internal surface quality is critical, the manufacturing route and verification strategy should be established before printing.
Inspection and Qualification of Additively Manufactured Components
Inspection and qualification are central to metal additive manufacturing in demanding oil and gas applications. The required evidence depends on the component’s function, criticality, operating environment and applicable contractual, technical or regulatory requirements.
Dimensional inspection
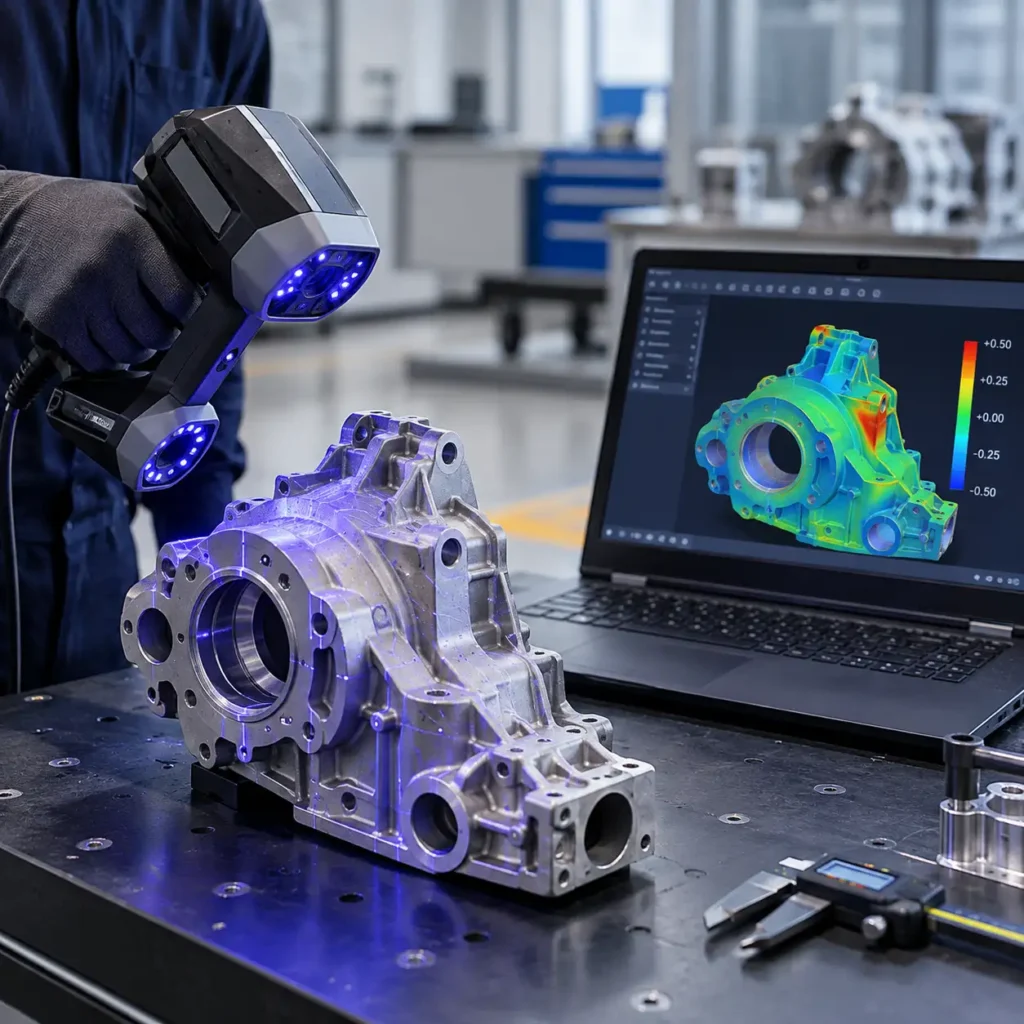
Dimensional verification may involve coordinate measurement, optical 3D scanning or other suitable metrology methods.
External scan-to-CAD comparison can identify geometric deviations on accessible surfaces. It cannot, by itself, establish the integrity of enclosed passages or the absence of internal material defects.
Non-destructive testing
Depending on the component and acceptance criteria, appropriate non-destructive testing (NDT) methods may be used to investigate discontinuities.
Industrial computed tomography can provide information about certain internal features, but its suitability depends on component size, material, geometry, resolution and the defects that must be detected. No single inspection method is appropriate for every part.
Pressure and functional testing
Relevant testing may include pressure-integrity, leakage, hydraulic-performance or other application-specific assessments. Rotating components may require additional mechanical and dynamic evaluation.
The testing programme should follow the component’s intended service and failure consequences, rather than relying on a generic checklist for all printed components.
Standards and qualification frameworks
API Standard 20S addresses qualification and production controls for metallic additive manufacturing in petroleum and natural gas applications. DNV-ST-B203 provides a framework for additive manufacturing quality and qualification.
These references can help engineering teams define relevant controls, documentation, inspection and acceptance requirements. Their applicability must be established for each component and project.
Mentioning a standard does not mean that a supplier, manufacturing facility or component is certified to it. Any required certification or qualification must be supported by the relevant evidence.
When Is Metal Additive Manufacturing the Right Choice?
LPBF should be compared with the most appropriate conventional manufacturing alternative. The decision should consider technical feasibility, total delivered cost, production volume, inspection requirements and qualification effort.
| Consideration | LPBF may be attractive when… | Conventional manufacturing may be preferable when… |
|---|---|---|
| Geometry | Complex internal passages are difficult to machine or assemble | Features are simple and accessible |
| Production volume | Specialised, low-volume parts are required | High-volume production benefits from established tooling |
| Integration | Several parts can be combined without compromising serviceability | Separate parts are easier to inspect, repair or replace |
| Material utilisation | Conventional machining would remove substantial material | The existing process already uses material efficiently |
| Surface finish | Required surfaces can be finished and verified | Extensive internal finishing would be difficult |
| Qualification | A suitable qualification pathway can be established | An established qualified process is available |
| Component size | The design fits the available build envelope | The component exceeds practical process dimensions |
The comparison should include tooling, machine time, material, post-processing, inspection, qualification, lead time and expected production volume.
The shortest printing cycle is not necessarily the shortest qualified delivery route. For critical applications, inspection, testing and approval can represent a substantial part of the overall schedule.
A Practical Engineering Workflow for Pumps, Valves and Flow Components
A structured assessment helps identify manufacturing risks before significant design or production resources are committed.
Step 1: Define operating requirements
Document the component’s function, pressure and temperature conditions, fluid properties, loading, dimensional requirements and expected service life.
Identify relevant industry specifications and restrictions on materials or manufacturing routes.
Step 2: Establish the manufacturing baseline
Review the existing production method and the reason an alternative is being considered. Determine whether the opportunity relates to geometry, supply availability, assembly complexity, material utilisation or production volume.
When an existing component is damaged or its original CAD model is unavailable, reverse engineering may help establish the geometry required for further engineering assessment. The reconstructed model must still be reviewed against design intent and service requirements.
Step 3: Evaluate additive manufacturing feasibility
Assess build size, material availability, orientation, support strategy, powder removal, finishing and inspection accessibility.
Reject or redesign features that cannot be manufactured, cleaned or verified adequately.
Step 4: Develop and assess the design
Use CAD, CFD and FEA where appropriate to investigate proposed changes. Compare the results with the baseline design and consider manufacturing variability.
Step 5: Plan production and post-processing
Define the build approach, machining allowances, heat treatment, surface finishing, cleaning and dimensional verification requirements.
Step 6: Establish qualification and acceptance criteria
Determine the evidence needed to demonstrate conformity. Depending on the application, this may include material testing, NDT, pressure testing, functional testing and documented traceability.
Step 7: Compare the complete manufacturing route
Evaluate additive manufacturing against casting, machining or fabrication using total cost, lead time, technical risk, serviceability and qualification effort.
The preferred route should be selected on the strength of this assessment—not simply because the component can be printed.
Supporting Oil and Gas Engineering in Australia
Australian oil and gas operations require manufacturing decisions that account for equipment reliability, specialised component requirements and practical industrial supply-chain constraints.
For suitable applications, metal additive manufacturing can support engineering development, low-volume production and the investigation of alternative component geometries.
E-Metal3D provides information on its Metal 3D Printing, Engineering Solutions and 3D Scanning Services for Australian industrial customers.
These service areas are relevant to workflows involving component assessment, geometry reconstruction, design development and additive manufacturing feasibility. The appropriate scope depends on the requirements of each project.
For an overview of the sector, visit E-Metal3D’s Oil and Gas industry page.
Component suitability, inspection requirements and qualification responsibilities should always be established for the individual application.
Conclusion
Metal additive manufacturing offers opportunities for selected oil and gas pump components, valve-related parts and complex flow-handling assemblies. Its strongest applications often involve specialised geometries that are difficult to manufacture conventionally, including integrated manifolds and internal passages.
Successful implementation requires more than the ability to print a complex shape. Hydraulic performance, structural integrity, material behaviour, surface finish, powder removal, inspection accessibility and qualification must be considered together.
For Australian engineering teams, LPBF should be evaluated as one manufacturing option within a broader technical and commercial decision. The right choice is the process that meets the component’s functional and acceptance requirements with an appropriate level of risk—not necessarily the process that offers the greatest geometric freedom.
Discuss an industrial component with E-Metal3D
If your team is evaluating a pump component, valve-related part or complex flow geometry for additive manufacturing, contact E-Metal3D to discuss the design requirements and available engineering and manufacturing pathways.
Can metal 3D printing manufacture oil and gas pump impellers?
Selected impeller designs can be manufactured using metal additive manufacturing. Suitability depends on geometry, material properties, surface finishing, dynamic balance, fatigue performance and the required qualification and testing programme.
Are 3D printed valve bodies suitable for high-pressure applications?
Some additively manufactured valve components may be suitable for pressure-related applications when their design, material, manufacturing process, inspection and testing satisfy the applicable requirements. Printability alone does not establish pressure integrity or service approval.
What is the advantage of LPBF for internal flow channels?
LPBF can produce certain complex internal passages without conventional drilling or assembly operations. This may enable compact designs or integrated manifolds, provided the channels can be manufactured, cleaned, inspected and verified.
Which materials are used for oil and gas additive manufacturing?
316L stainless steel and selected nickel-based alloys may be considered for particular applications. The appropriate material depends on the fluid environment, temperature, mechanical loading, corrosion mechanisms and qualified manufacturing route.
Can CFD predict the performance of a 3D printed flow component?
CFD can help compare design alternatives and investigate flow behaviour. Predictions depend on modelling assumptions and should account for manufactured geometry and surface condition. Physical testing may still be necessary.
Does metal additive manufacturing eliminate the need for machining?
No. Precision bores, threads, sealing faces and connection features may require machining or other finishing after printing. The required operations depend on the design and acceptance criteria.
How are additively manufactured oil and gas components inspected?
Depending on the application, inspection may include dimensional metrology, material testing, non-destructive examination, pressure testing and functional assessment. The inspection plan should be defined by the component’s requirements and criticality.
Which standards are relevant to metal additive manufacturing in oil and gas?
API Standard 20S and DNV-ST-B203 are relevant references for metallic additive manufacturing qualification and quality frameworks. Applicability depends on the project and component. Referencing a standard does not establish certification or approval.